If you’ve ever worked with a piercing mill—whether you’re a plant supervisor, maintenance technician, or someone who sources critical wear parts for tube and pipe manufacturing—you know downtime from a single faulty spare can derail an entire production shift. For 12 years, I’ve run a company that supplies piercing mill wear spare parts: rolls, guide shoes, mandrel bars, and bearing housings, all engineered to withstand the extreme heat, pressure, and friction of seamless tube production. Over that time, I’ve seen two types of mistakes that cause the most avoidable safety incidents: cutting corners on personal protection when handling parts, or neglecting basic inspection and storage protocols for these heavy, often sharp, components. This post breaks down the non-negotiable safety precautions I’ve drilled into our team and share with every client, because handling piercing mill wear spare parts isn’t just about inventory management—it’s about protecting the people who work around them every day. Piercing Mill Wear Spare Parts
First, let’s ground this in why these parts are uniquely hazardous. A primary piercing mill’s top and bottom guide rolls, for example, can weigh 80 to 120 kilograms each, with machined edges and sharp corners from their manufacturing process. Guide shoes, designed to stabilize the steel billet during piercing, have hardened steel contact surfaces that can cut through thick work gloves if handled incorrectly. Even smaller parts, like the set screws that secure rolls to their shafts, often have unthreaded edges that can catch on gloves or clothing, leading to trips or falls in cluttered maintenance bays. I once had a new warehouse worker skip safety training and try to carry a pair of guide rolls solo—he dropped one on his foot, breaking a metatarsal and costing our client three days of delayed part delivery. That incident taught me that every precaution, no matter how small, is tied to both worker safety and operational reliability.
The first set of precautions revolves around personal protective equipment (PPE), and I won’t mince words: generic work gloves or safety glasses won’t cut it here. Our team uses cut-resistant, heat-resistant gloves rated for level 5 cut resistance—standard work gloves, even leather, tear easily on the sharp edges of new mill parts, and thin disposable gloves offer zero protection. For heavy parts, we add steel-toe boots with metatarsal guards, not just regular work boots; a 100-kilogram roll falling onto an unguarded foot can cause permanent injury. We also mandate full face shields for anyone removing parts from wooden crates or metal packaging, because old packaging nails or broken metal brackets can fly loose when pried open. I’ve seen clients skip the face shield and get a metal splinter in their eye that required emergency surgery, so this isn’t a suggestion—it’s a rule. One note: some technicians opt for lightweight gloves for small parts like set screws, but even a tiny unthreaded bolt can cause a laceration if handled without proper gear.
Next, storage and lifting protocols, which are often overlooked because these parts are “just inventory.” Piercing mill wear spare parts are heavy, and improper lifting is the leading cause of musculoskeletal injuries in maintenance teams. We never allow a single person to lift a component over 50 kilograms; even a 60-kilogram mandrel bar can cause a herniated disc if bent incorrectly. Our team uses mobile lifting aids—adjustable cranes, pallet jacks with wide forks, and suction cups for smooth, round parts like guide rolls—for every component over 20 kilograms. We also store parts in climate-controlled, dry racks, not on the floor or in unventilated sheds. Why? These parts are often coated with anti-corrosion oil for shipping, and moisture can cause rust that makes handling slipperier. I once visited a client who stored their guide rolls on a damp concrete floor; a roll slid off a stack during loading, crushing a forklift operator’s leg. That’s a preventable accident, and proper storage reduces that risk. We also label every rack with the part’s weight and maximum safe lifting limit for our clients, because even experienced technicians can underestimate how heavy a new roll is.
Inspection is another critical safety step, before parts even reach the mill floor. Many clients assume all new spare parts are safe to install, but manufacturing defects are common—and those defects can cause catastrophic mill failures. For example, a guide roll with a micro-crack in its outer shell, undetectable to the naked eye before installation, can shatter during a piercing cycle, sending shards of hardened steel at speeds over 100 kilometers per hour. That’s a death sentence if a technician is nearby. Our team inspects every part before shipment, and we train our clients to do the same on delivery. What do we check? For rolls: surface cracks, uneven hardness (we use a portable hardness tester to confirm matches the manufacturer’s spec), and bent shafts. For guide shoes: sharp edges on machined surfaces, missing set screws, and warping from heat during testing. We also reject parts that have been dropped during shipping—even a small drop can cause internal damage that won’t show until the mill is running. One client told me they installed a part that passed their basic visual check, but it had a hidden crack; the mill shut down for 12 hours, and a technician was hit by a shard when it failed. That’s why thorough inspection isn’t just about quality control—it’s safety.
Handling during installation and removal is another area with specific precautions. When removing old parts from the mill, technicians must lock out/tag out (LOTO) the mill before starting work—this is standard, but I’ve seen clients skip LOTO because the mill is “cool” and hasn’t run in hours. The problem is, hydraulic lines can still pressurize, or a motor can accidentally turn on, causing a part to fall. We require all clients to follow OSHA’s LOTO guidelines every time they handle any piercing mill part, new or used. When removing old rolls, we use pullers designed specifically for piercing mill shafts, not pry bars; pry bars can slip, sending a technician into the mill structure. For installing new parts, we use alignment tools to ensure rolls are seated correctly—misaligned rolls can wear out faster, but more importantly, they can cause the billet to eject violently, endangering nearby workers. Our sales team regularly visits clients’ mills to train maintenance teams on these tools, because we’ve seen too many injuries from makeshift methods.
One often-missed precaution is handling used parts before disposal. Many maintenance teams just throw old rolls or guide shoes in a scrap bin, but these parts often have sharp, worn edges and residual anti-corrosion oil that can cause slips or cuts. We advise clients to mark scrap parts with “sharp edges” and store them in a locked bin, not accessible to general workers, before sending them to a metal recycler. I once had a client’s warehouse worker cut their hand on a scrap guide shoe that wasn’t marked, leading to a week-long time off work. It’s a small step, but it prevents a lot of avoidable incidents.
Beyond the immediate safety steps, there’s a cultural angle that matters most. As a supplier, we don’t just sell parts—we share our 12 years of safety data with every client. We track every incident our team has seen, from cuts and falls to mill failures, and we make that data available to clients so they understand why each precaution exists. For example, we share a case study about a client that skipped LOTO and had a hydraulic hose burst, sending a roll flying across the mill floor, because context makes the rule stick, not just a “don’t do this.” We also require all our own warehouse staff to complete monthly safety refreshers, including hands-on lifting and inspection drills, because if our team models safe handling, our clients are more likely to follow suit.
I know some clients see these precautions as an extra cost—time spent inspecting, lifting aids, PPE, training—but the alternative is far more expensive. A single injury can cost a company in workers’ comp claims, downtime, and lost productivity. I’ve had clients tell me that investing in proper safety protocols reduced their incident rate by 85% in one year, and cut their mill downtime from part-related failures by 20%. That’s a return on investment that far outweighs the cost of a good pair of cut-resistant gloves or a mobile crane.
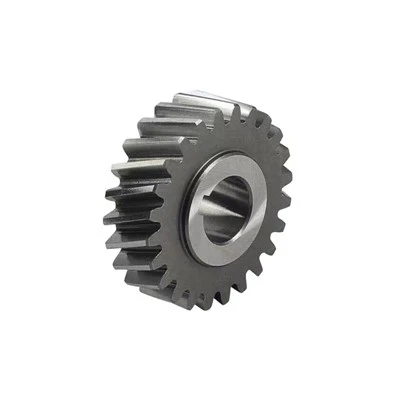
At the end of the day, handling piercing mill wear spare parts comes down to respect for the equipment and the people who work with it. For our team, every part we ship isn’t just a component—it’s a critical piece that needs to be handled safely, from the warehouse floor to the mill floor. If you’re a maintenance supervisor, plant manager, or anyone sourcing these parts and want to review your safety protocols, or if you need reliable, tested piercing mill wear spare parts with built-in safety documentation, we’re here to help. Don’t hesitate to reach out to connect for a discussion tailored to your operation’s needs.
Mill and Mill Auxiliary Parts References
- Occupational Safety and Health Administration (OSHA), Lockout/Tagout Standard for Heavy Machinery (29 CFR 1910.147)
- Steel Fabricators Association of America, Safety Guidelines for Handling Large Industrial Machinery Components
- Journal of Manufacturing Safety, Incident Analysis of Piercing Mill Component Failures (2018)
- American Society of Mechanical Engineers (ASME), Standard for Wear Part Inspection and Testing for Metal Forming Equipment
Jingjiang Jingyi Metallurgical Technology Co., Ltd.
With abundant experience, we are one of the most reliable piercing mill wear spare parts manufacturers and suppliers in China. We warmly welcome you to wholesale customized piercing mill wear spare parts made in China here from our factory. If you have any enquiry about quotation, please feel free to email us.
Address: No.5 Jianghe Road, Xinqiao Town, Jingjiang City, Jiangsu Province
E-mail: Lcbin1974@163.com
WebSite: https://www.jymetallurgical.com/
